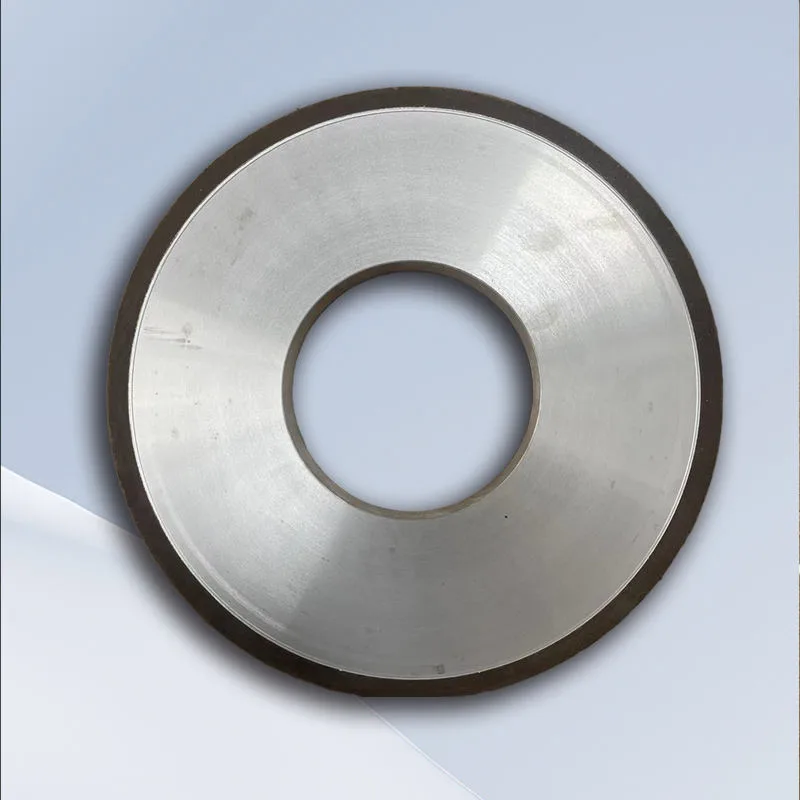
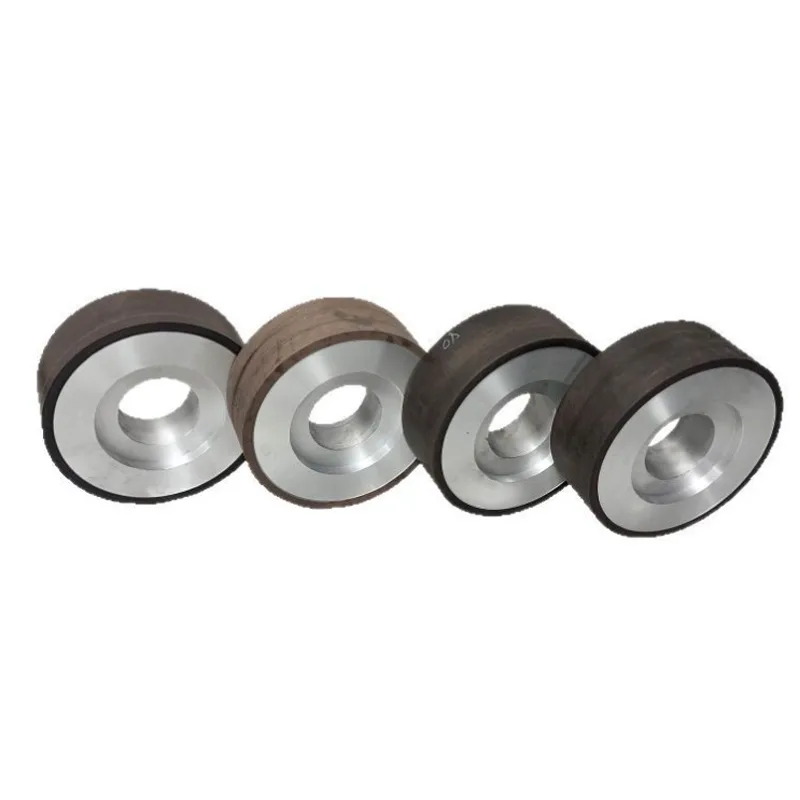
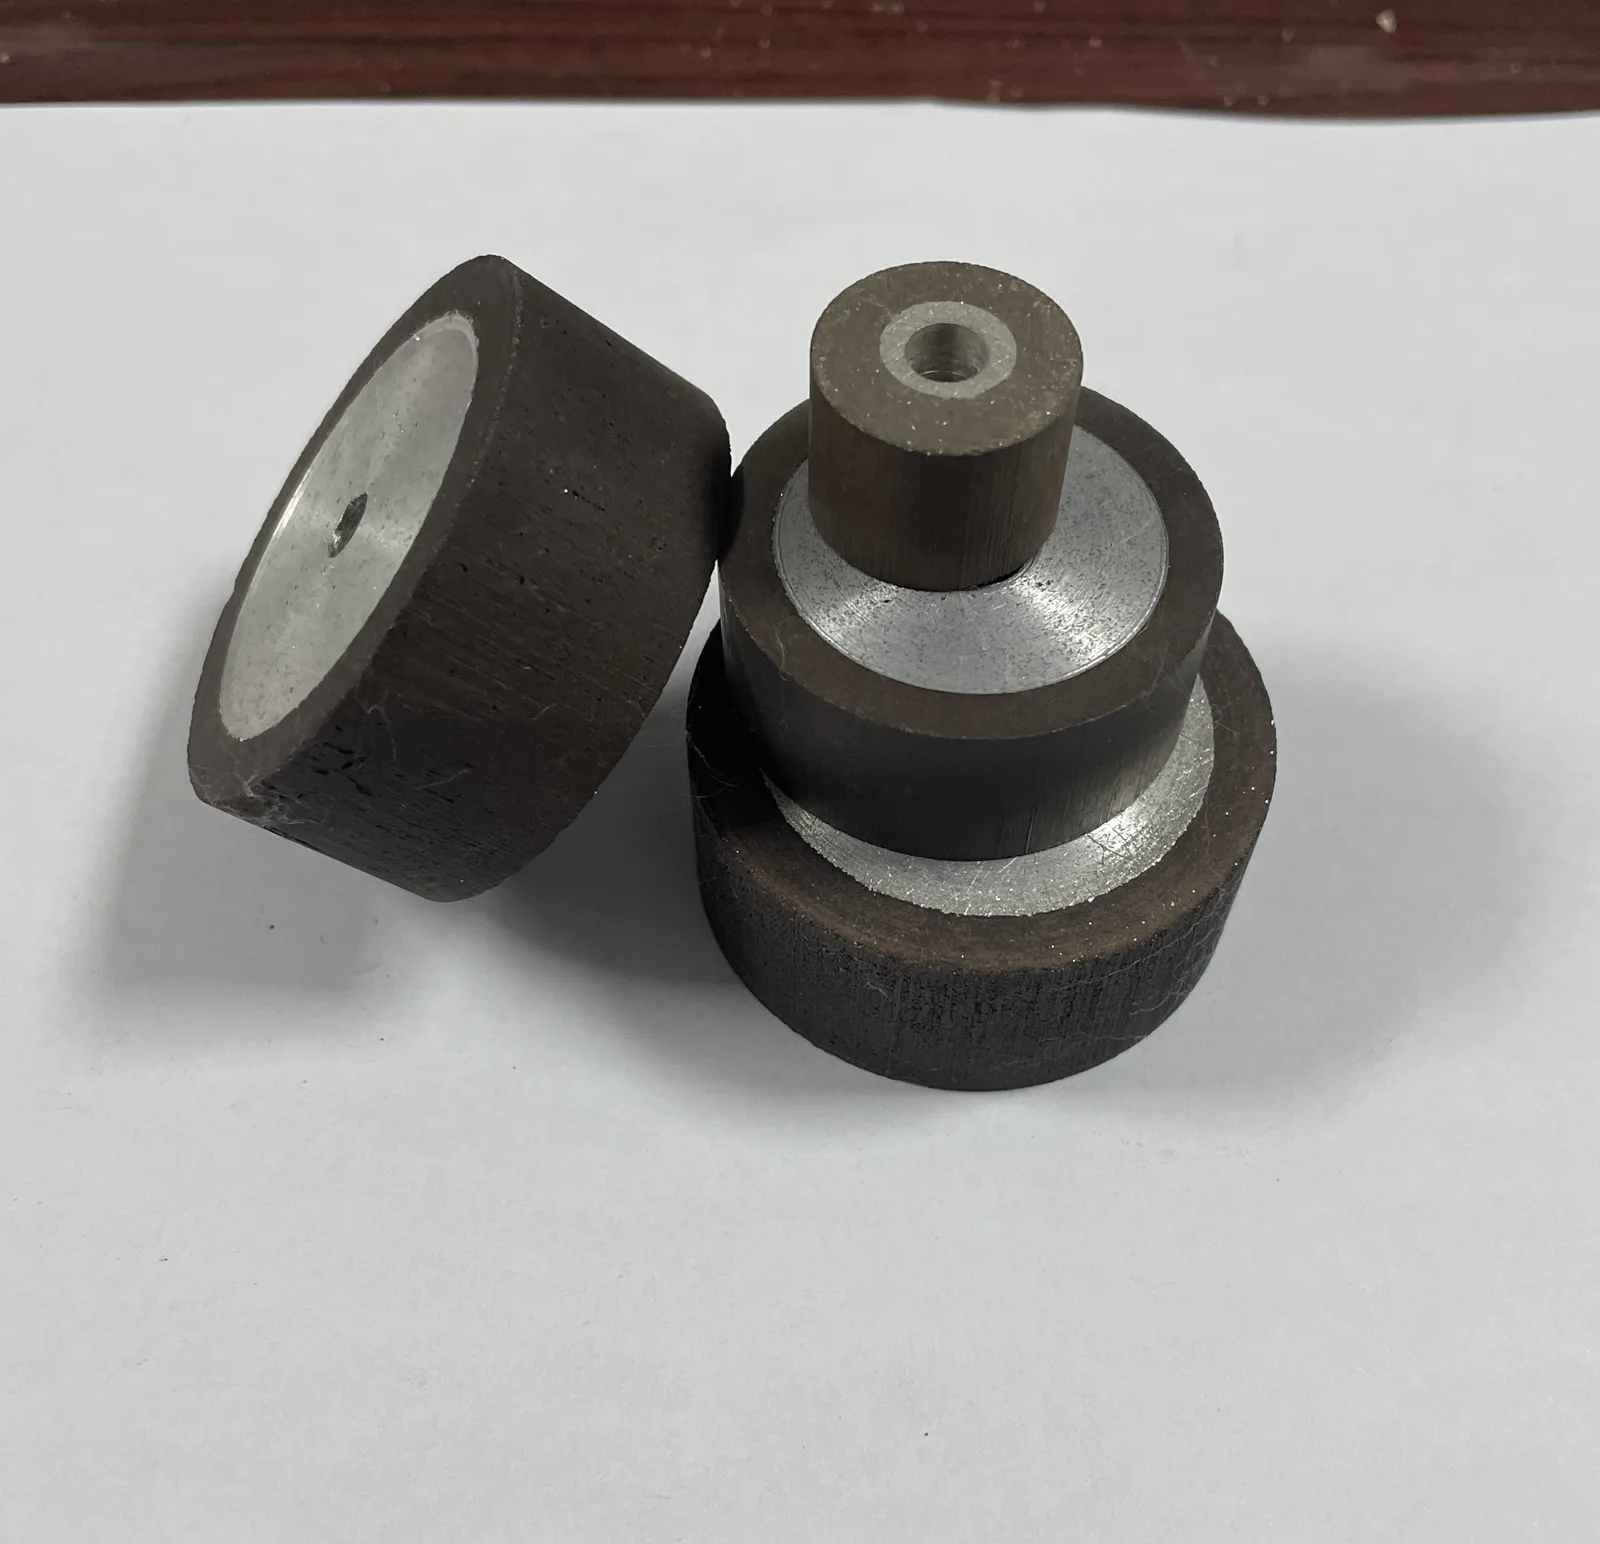
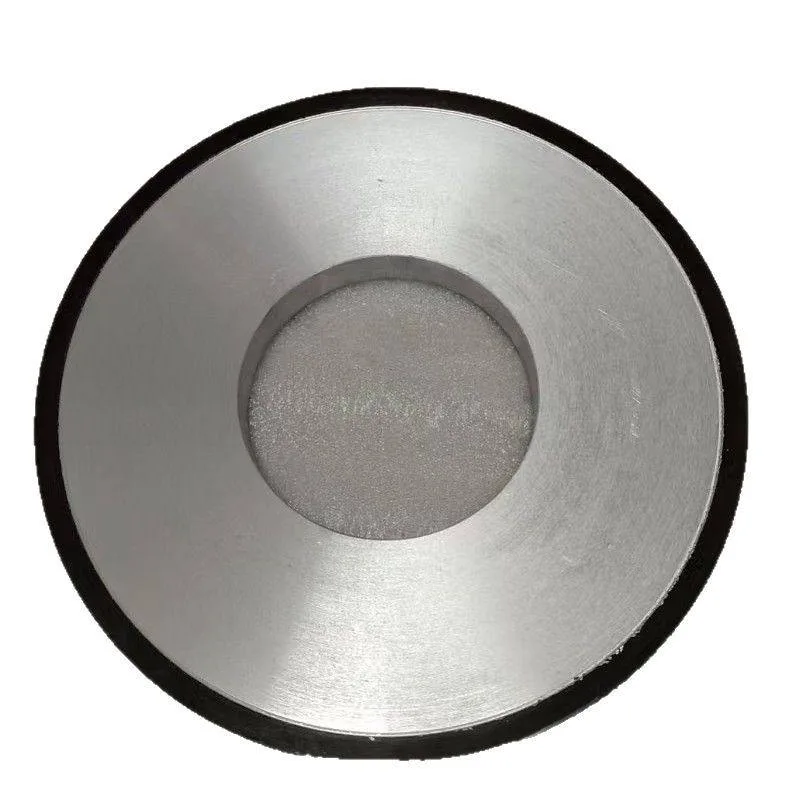
Resin bond diamond wheels from Fengzuan deliver sharp, cool cutting and a fine surface finish. The resin matrix releases worn diamond grains steadily, so the wheel keeps exposing fresh cutting edges with low grinding heat. That makes a resin bond diamond wheel the standard choice for tungsten carbide tool grinding, sharpening and regrinding, and for precision work on ceramics, glass and other hard, brittle materials.
We produce every wheel in our own factory in Shijiazhuang, Hebei, China: cold pressing on hydraulic presses, resin curing, precision turning, dynamic balancing and truing. Wheels are made to your drawing, your sample or your current wheel marking.
Resin Bond Diamond Wheel Specifications
| Parameter | Range / option |
|---|---|
| Abrasive | Synthetic diamond (CBN available in the same bond) |
| Bond | Resin (B) |
| Outer diameter (D) | Ø10–850 mm |
| Thickness (T) / bore (H) | Made to your drawing / to suit your machine spindle |
| Abrasive layer (X) | 3–20 mm common; other depths to drawing |
| Grit | 80# – 3000# |
| Concentration | 50 – 150 |
| Shapes | 1A1, 6A2, 6A2T, 11A2, 12A2, 14E1, internal 1A8/1A1W and profiles to drawing |
| Coolant | Wet or dry grinding |
| Marking example | 1A1 D150 T10 X5 H32 · D/CBN 140/170 C75 B/V/R |
Shapes for Tool and Cutter Grinding
1A1 resin bond diamond wheel (straight / parallel)
The 1A1 straight wheel is used for peripheral grinding of carbide rods and blanks, cylindrical and surface grinding, and flute grinding on tool grinders. Our 1A1 parallel wheels are produced across the full diameter range, with layer depth chosen for your stock removal.
11A2 flaring cup wheel
The 11A2 flaring cup wheel is the classic shape for sharpening the clearance faces of carbide end mills, drills and cutters on tool and cutter grinders.
12A2 dish wheel
The 12A2 dish wheel reaches into flutes and gashes, and is used for rake-face and gash grinding of carbide tools and saw tips.
6A2 and 6A2T cup wheels
6A2 and 6A2T straight cup wheels are used for face grinding of carbide inserts and flat surfaces where a wide, rigid contact face is needed.
14E1 V-edge wheel
The 14E1 wheel has a V-shaped edge for grinding grooves, threads, flutes and profiles. Angle and edge radius are made to your drawing.
Applicable Workpiece Materials
- Tungsten carbide tools, inserts, rods and dies
- Technical ceramics such as alumina, zirconia and silicon nitride
- Glass and optical materials
- Semiconductor materials such as silicon and sapphire
- Tool and cutter grinding, sharpening and regrinding
Advantages of the Resin Bond
- Sharp, free cutting with low grinding heat, reducing thermal cracks on carbide
- Fine surface finish and good edge quality
- Reduced risk of edge chipping on brittle materials
- Suitable for both wet and dry grinding
- Easy to true and dress on the machine
- Wide choice of shapes, grits (80#–3000#) and concentrations (50–150)
Need a different bond? For PCD, PCBN and profile holding see vitrified bond diamond wheels; for long life on ceramics and glass see metal (bronze) bond diamond wheels. Application advice: diamond wheels for carbide tool grinding.
Ordering, Samples and Delivery
- MOQ: 15 pcs per specification
- Samples: produced within 30 days; sample cost and freight are charged
- Bulk production: within 45 days after drawing confirmation
- Payment: PayPal · Trade term: FOB · Shipping: international express
- Export markets served: Russia, USA, Germany, UAE and Qatar
What to send for a fast quote
- Shape code and full size (D, T, X, H, layer width, angles or radii)
- Diamond or CBN, grit and concentration (if known)
- Bond preference: resin (B), vitrified (V) or bronze/metal
- Workpiece material and machine model, wet or dry grinding
- Quantity, required lead time and destination
Frequently Asked Questions
Can resin bond diamond wheels be used dry?
Yes. Our resin bond diamond wheels can be used for both wet and dry grinding. Wet grinding with coolant generally gives a cooler cut and longer wheel life; tell us your process and we will match the specification.
Which grit should I choose for carbide tool sharpening?
Coarser grits remove stock faster, finer grits give a sharper edge and better finish. We produce grits from 80# up to 3000#. Send your tool type and required finish and we will recommend a grit for roughing and one for finishing.
What concentration do you recommend?
Concentration is available from 50 to 150. Higher concentration holds form and edge better on narrow contact areas; lower concentration cuts more freely on wide contact areas. We set it according to your shape and material.
Can you copy my existing wheel?
Yes. Send a photo of the wheel and its marking (for example 1A1 D150 T10 X5 H32 D126 C75 B) or a drawing, and we will make a matching wheel.
What is the minimum order quantity?
The MOQ is 15 pcs per specification. Samples can be made within 30 days; sample cost and freight are charged.
Get a Resin Bond Diamond Wheel Quote
Send your drawing, current wheel marking or application details. Our team will recommend shape, grit and concentration and send a quotation. Email lw892398@gmail.com or WhatsApp +86 13282830167. We reply within 24 hours (China Standard Time, UTC+8).